
MIG/MAG welding, also known as gas metal arc welding, encompasses two variations: metal inert gas welding (MIG) and metal active gas welding (MAG). It stands as the most commonly utilized welding process, offering exceptionally high welding speeds. This technique can be employed manually, mechanized, or with robot support.
In MIG/MAG welding, an arc is ignited when a filler metal or welding wire comes into contact with the component. The consumable wire serves as an allowance.
To safeguard the arc from reactive oxygen in the environment, a "shielding gas" also flows through the gas nozzle. This gas suppresses oxygen during welding, thereby preventing oxidation on the arc and the weld pool.
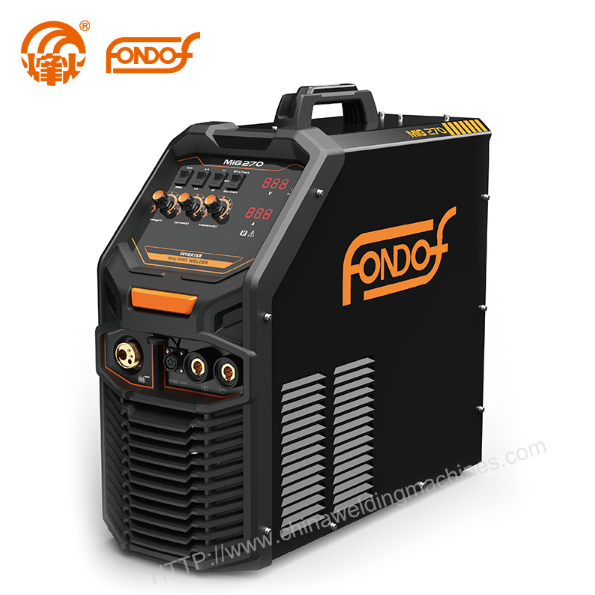
MAG welding utilizes active gases like pure CO2 or mixed gases (argon, CO2, O2) in different compositions, which are highly reactive. The MAG process is employed for welding unalloyed, low-alloy, and high-alloy materials.
In contrast, MIG welding utilizes inert, or unreactive, gases such as pure argon and helium, or mixtures of argon and helium. This process is suitable for welding materials such as aluminum, copper, magnesium, and titanium.
(1) Mains connection
(2) Power source
(3) Hosepack
(4) Grounding cable
(5) Welding torch
(6) Ground terminal
(7) Workpiece
(8) Filler metal
(9) Shielding gas
MIG/MAG welder involves various arc types, which vary based on the level of amperage. In the low power range, the arc is prone to short circuits, while in the higher power range, it operates free of short circuits.
The arc initiates when there's brief contact between the wire electrode and the component. This results in a rapidly increasing short circuit current, causing the wire electrode to liquefy and detach a droplet. Following the short circuit, the arc rekindles. Dip transfer arc is employed in the lower power range for thinner sheets and facilitates welding in nearly any position. It's primarily utilized in the root pass.
The spray arc operates continuously without short circuits in the higher power range, making it suitable for welding thicker sheets. This enables high deposition rates and deep penetration.
The pulsed arc comprises a low-power base current phase and a high-power pulsing current phase without short circuits. This results in minimal spatter production. During the pulsing current phase, welding droplets are detached in a controlled manner via precisely dosed current pulses.
Even more powerful than the spray arc, the rotating arc is employed for thick sheets requiring high deposition rates. The welding droplet is transferred into the weld pool through a rotating motion. The rotating arc is also known as a high-performance arc.
The combined arc integrates a dip transfer arc and a pulsed arc. The pulsed arc phase generates necessary penetration and heat input, while the dip transfer arc phase aids in cooling the weld pool and simplifying its management.
The most commonly welded material in gas metal arc welding is steel. Additionally, aluminum and stainless steel alloys can also be effectively welded using MIG/MAG.
Copyright:@2020-2021

Comments Please sign in or sign up to post.
0
0 of 500 characters used